Conveyor Projects & Case Studies
Real-world sanitary conveyor systems designed, built, and installed by AQS — from freezer-rated marshmallow lines to high-capacity dairy accumulation systems. Spotlights open to the full story.
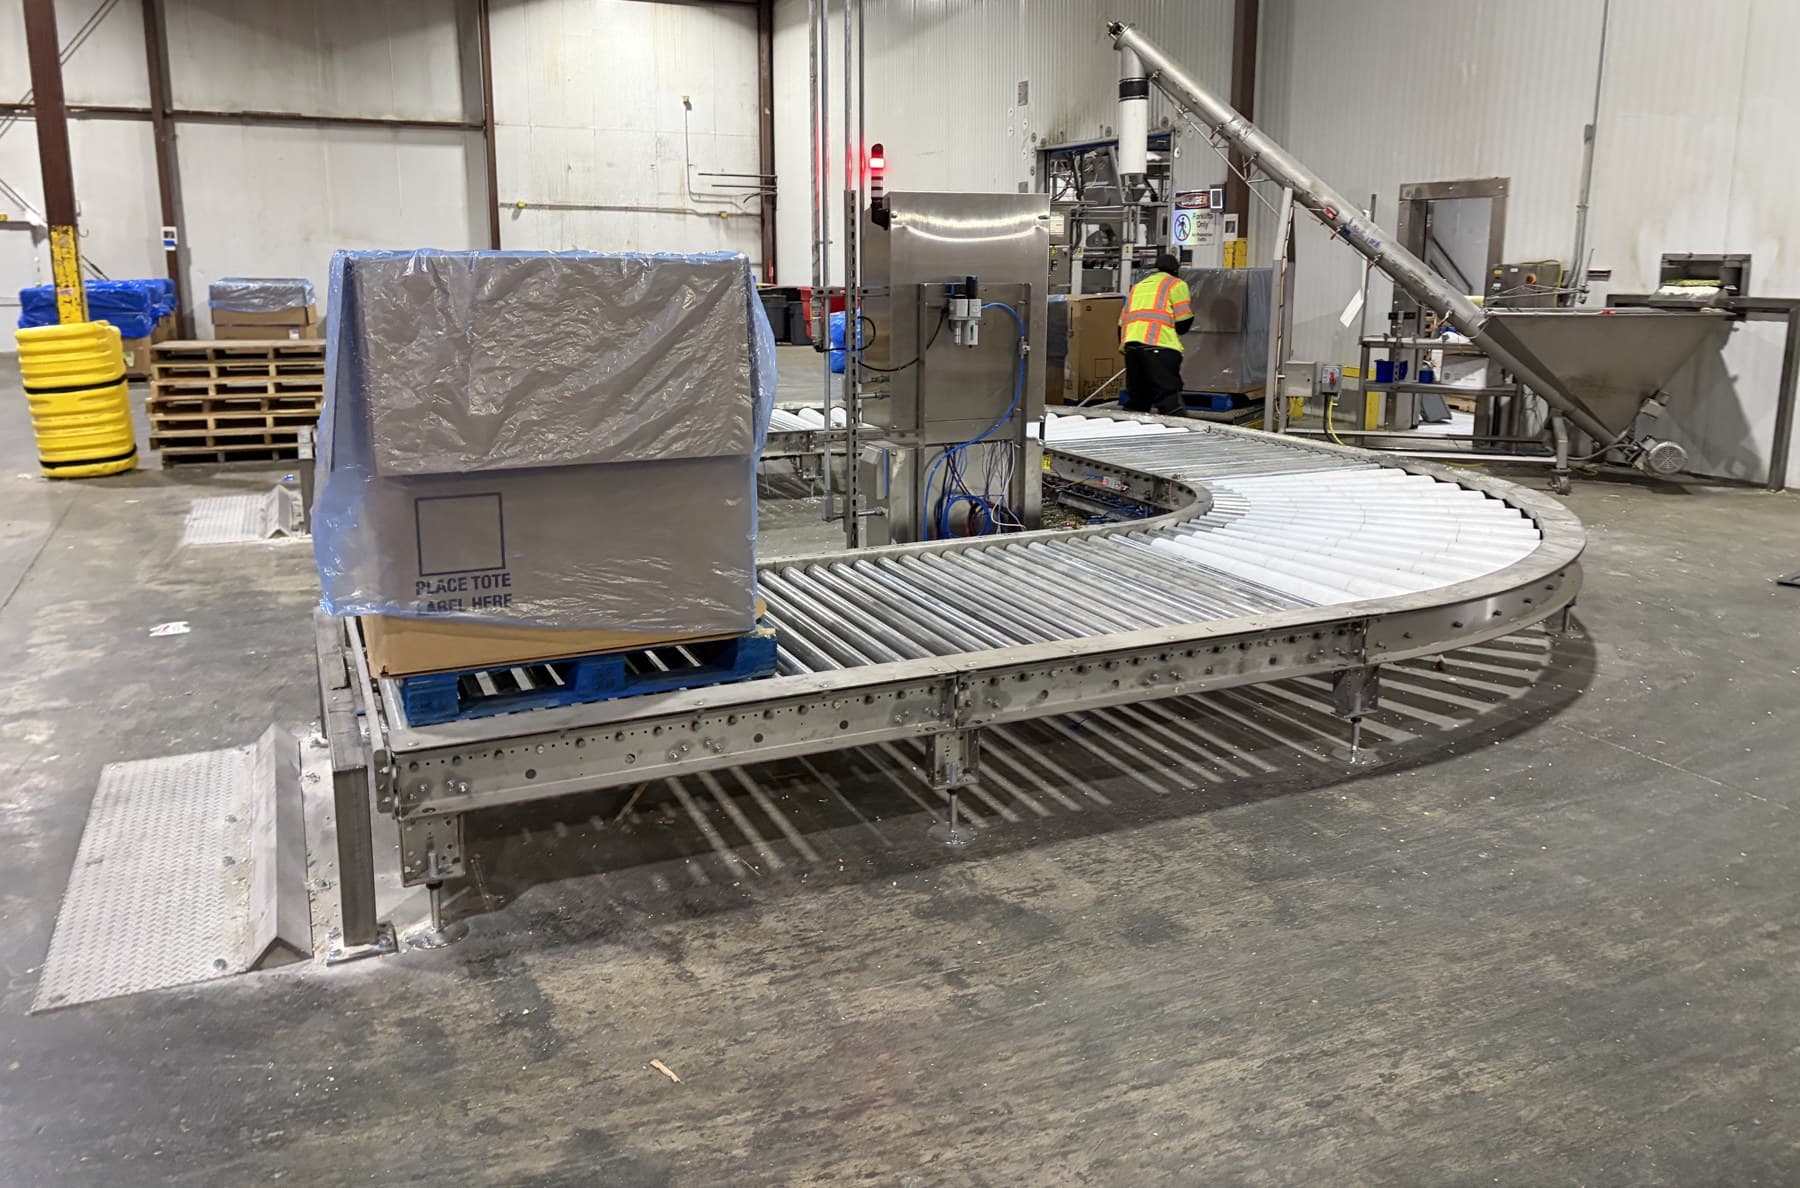
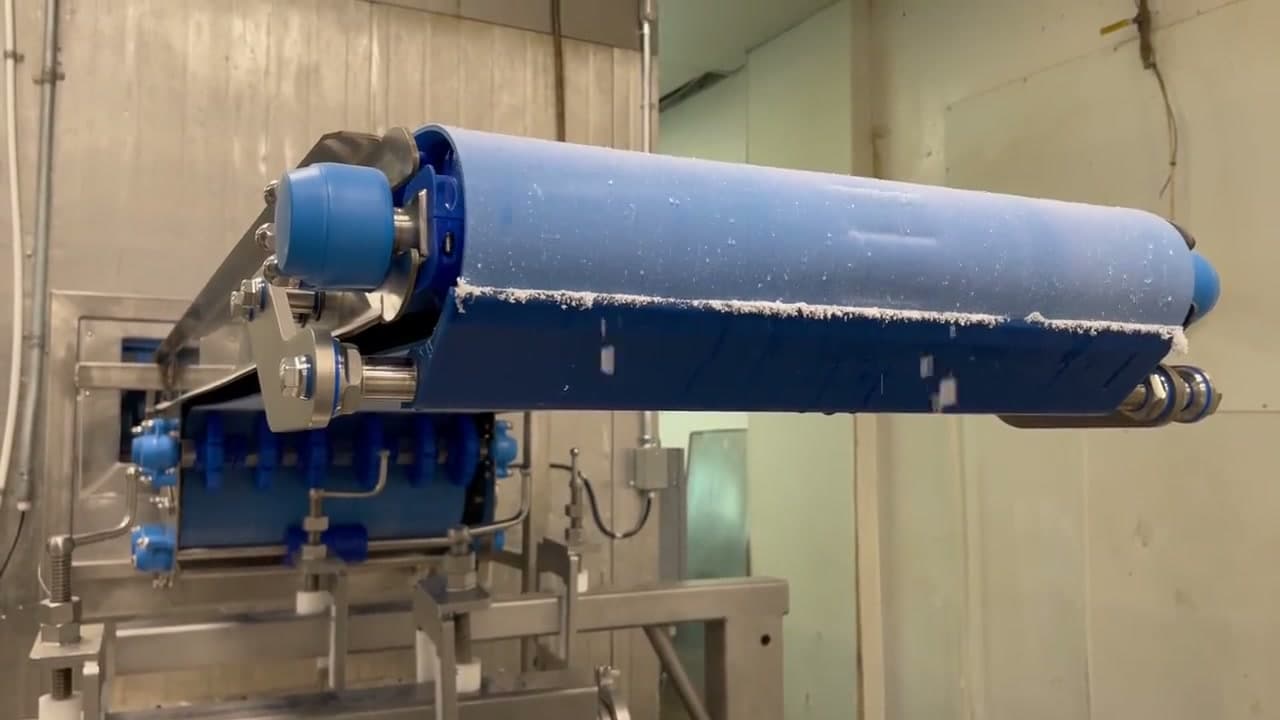
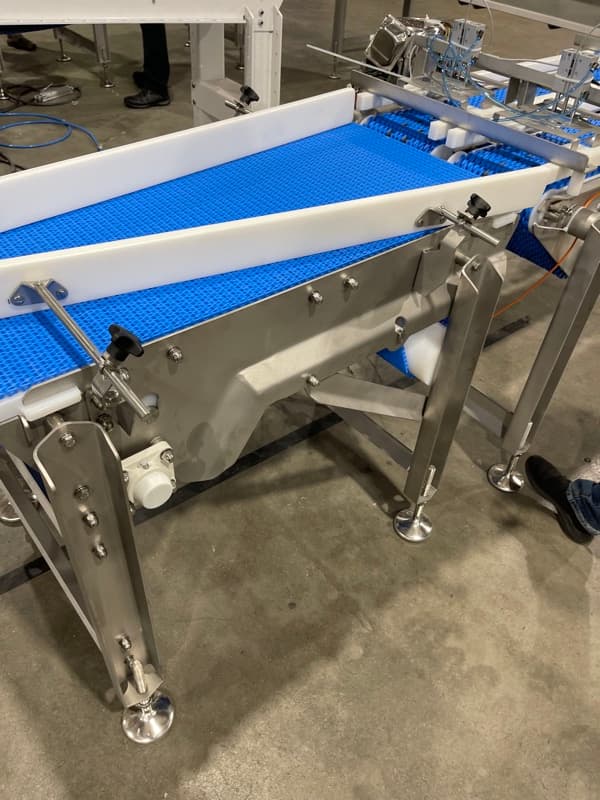
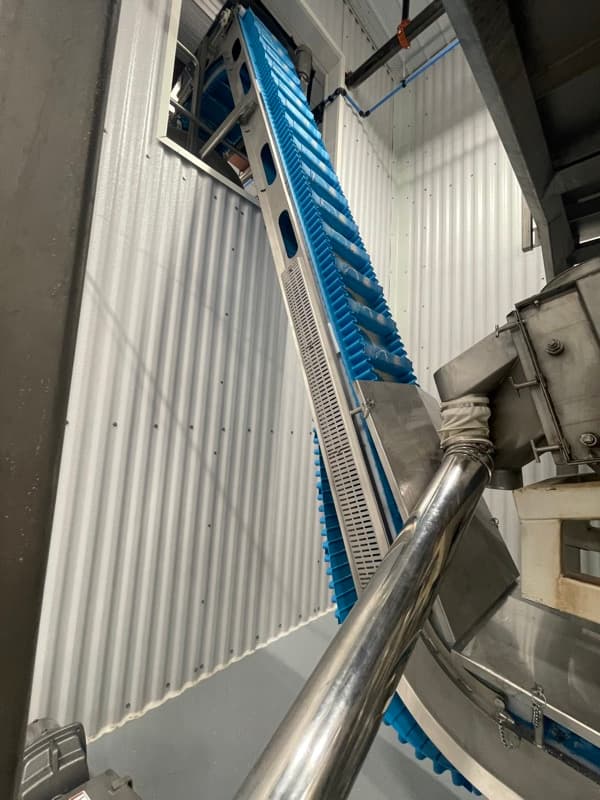
State-of-the-art sanitary conveyor systems for transporting hot extruded marshmallow through a freezer tunnel. Full washdown construction rated for extreme temperature cycling.
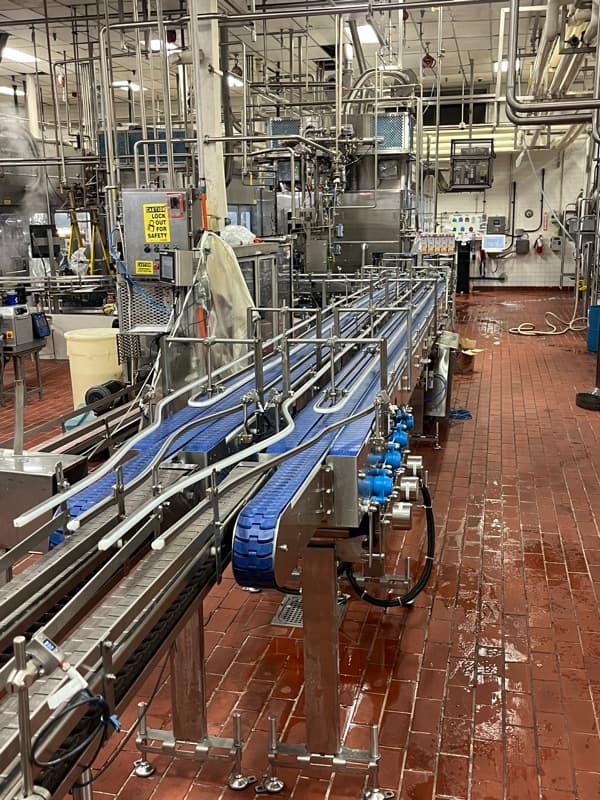
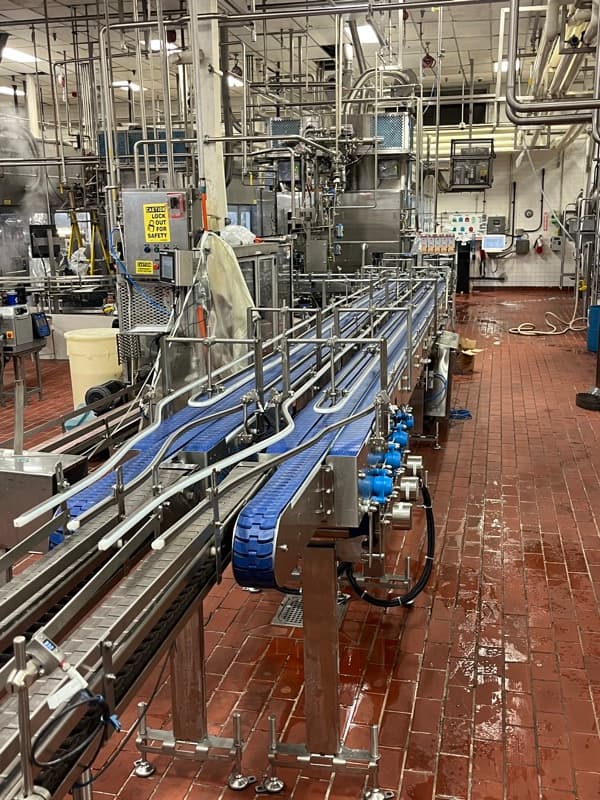
Advanced EQ70 accumulation conveyor installed at a major dairy production facility. Designed for active product accumulation with enhanced operational efficiency and stringent sanitation standards.
Conveyor Gallery
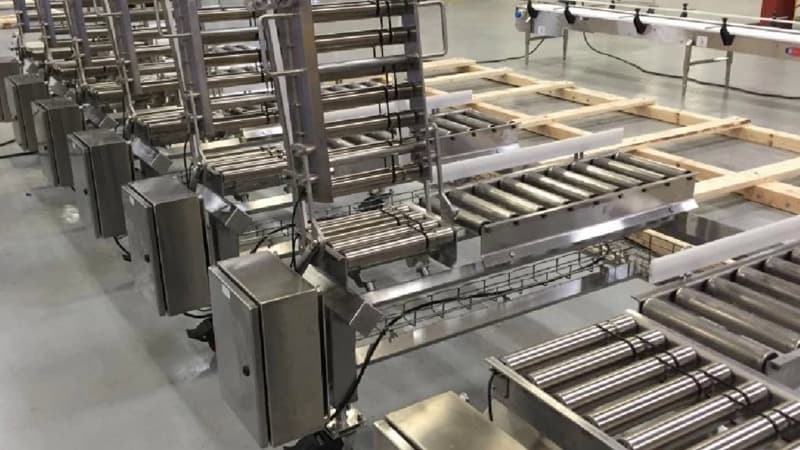
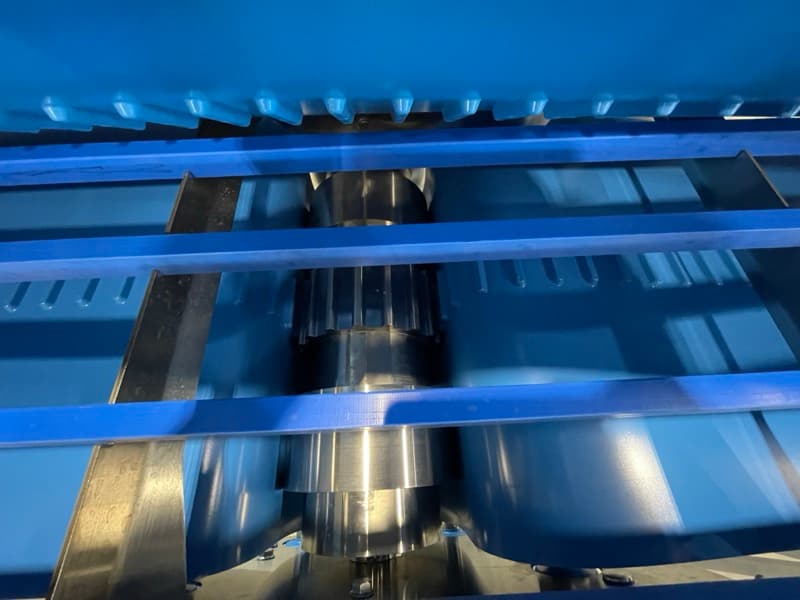
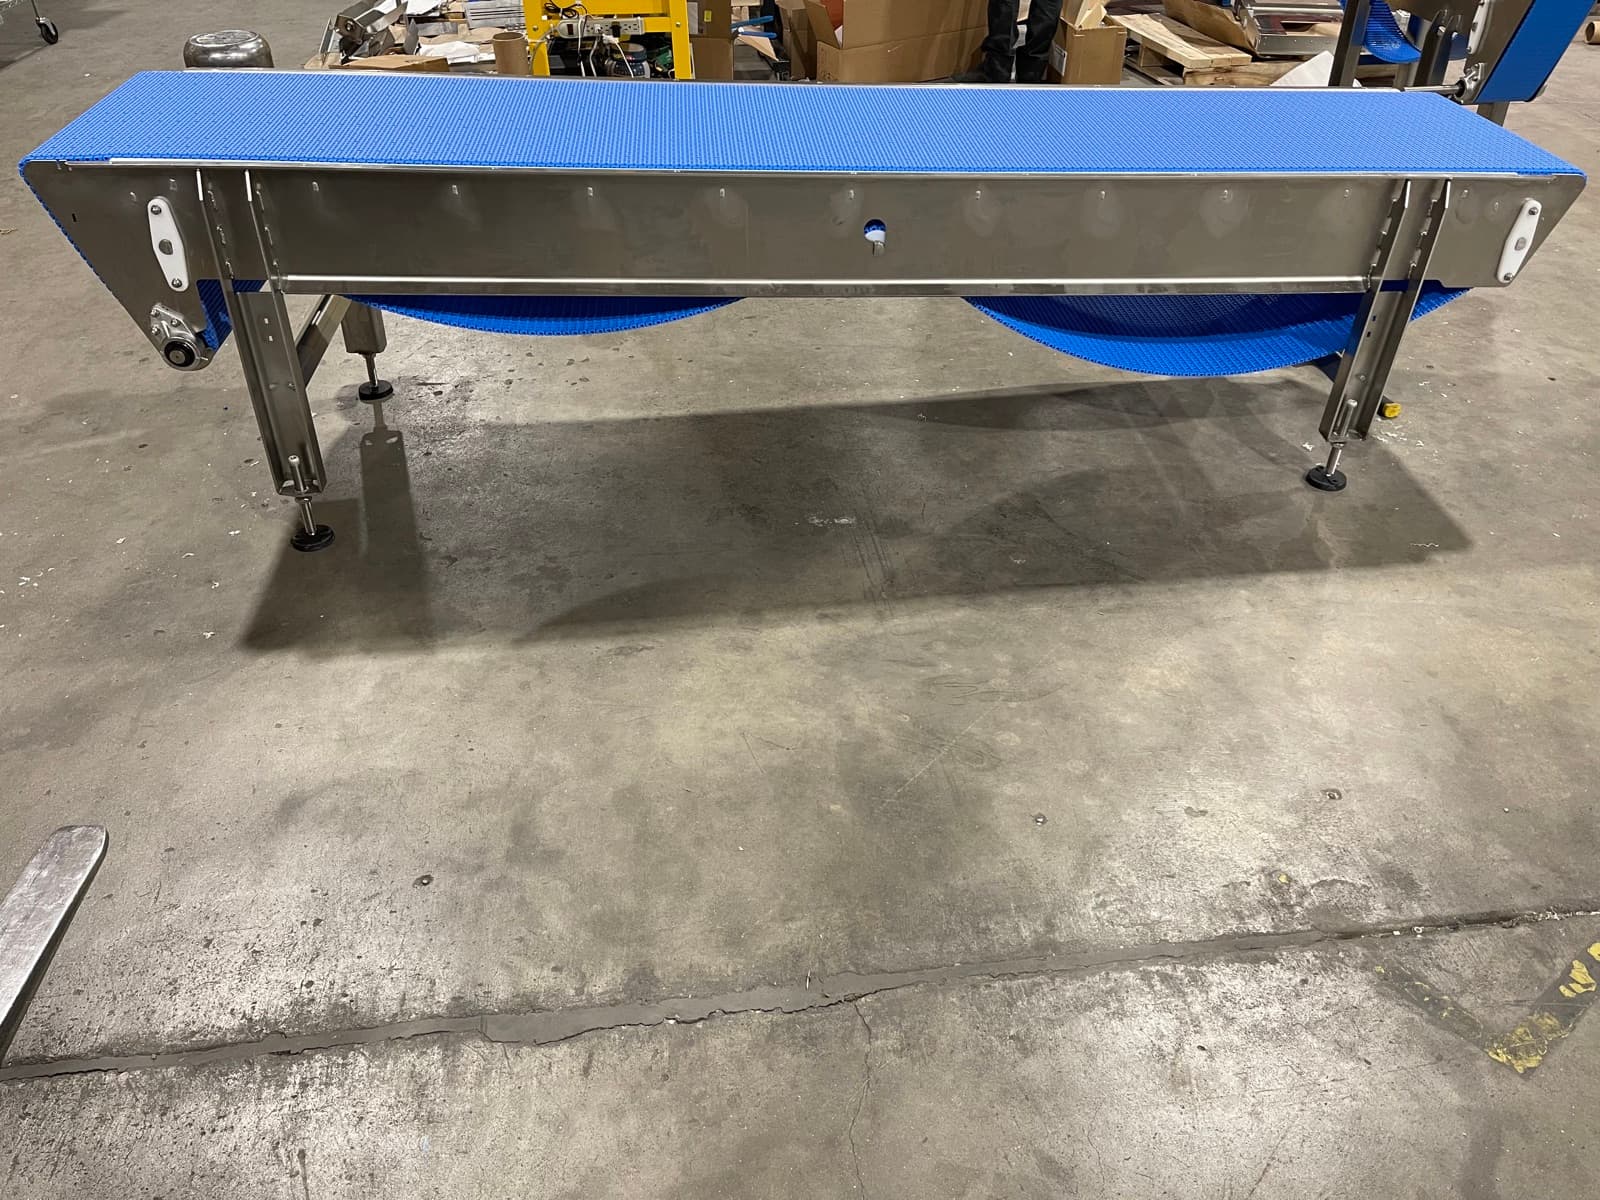
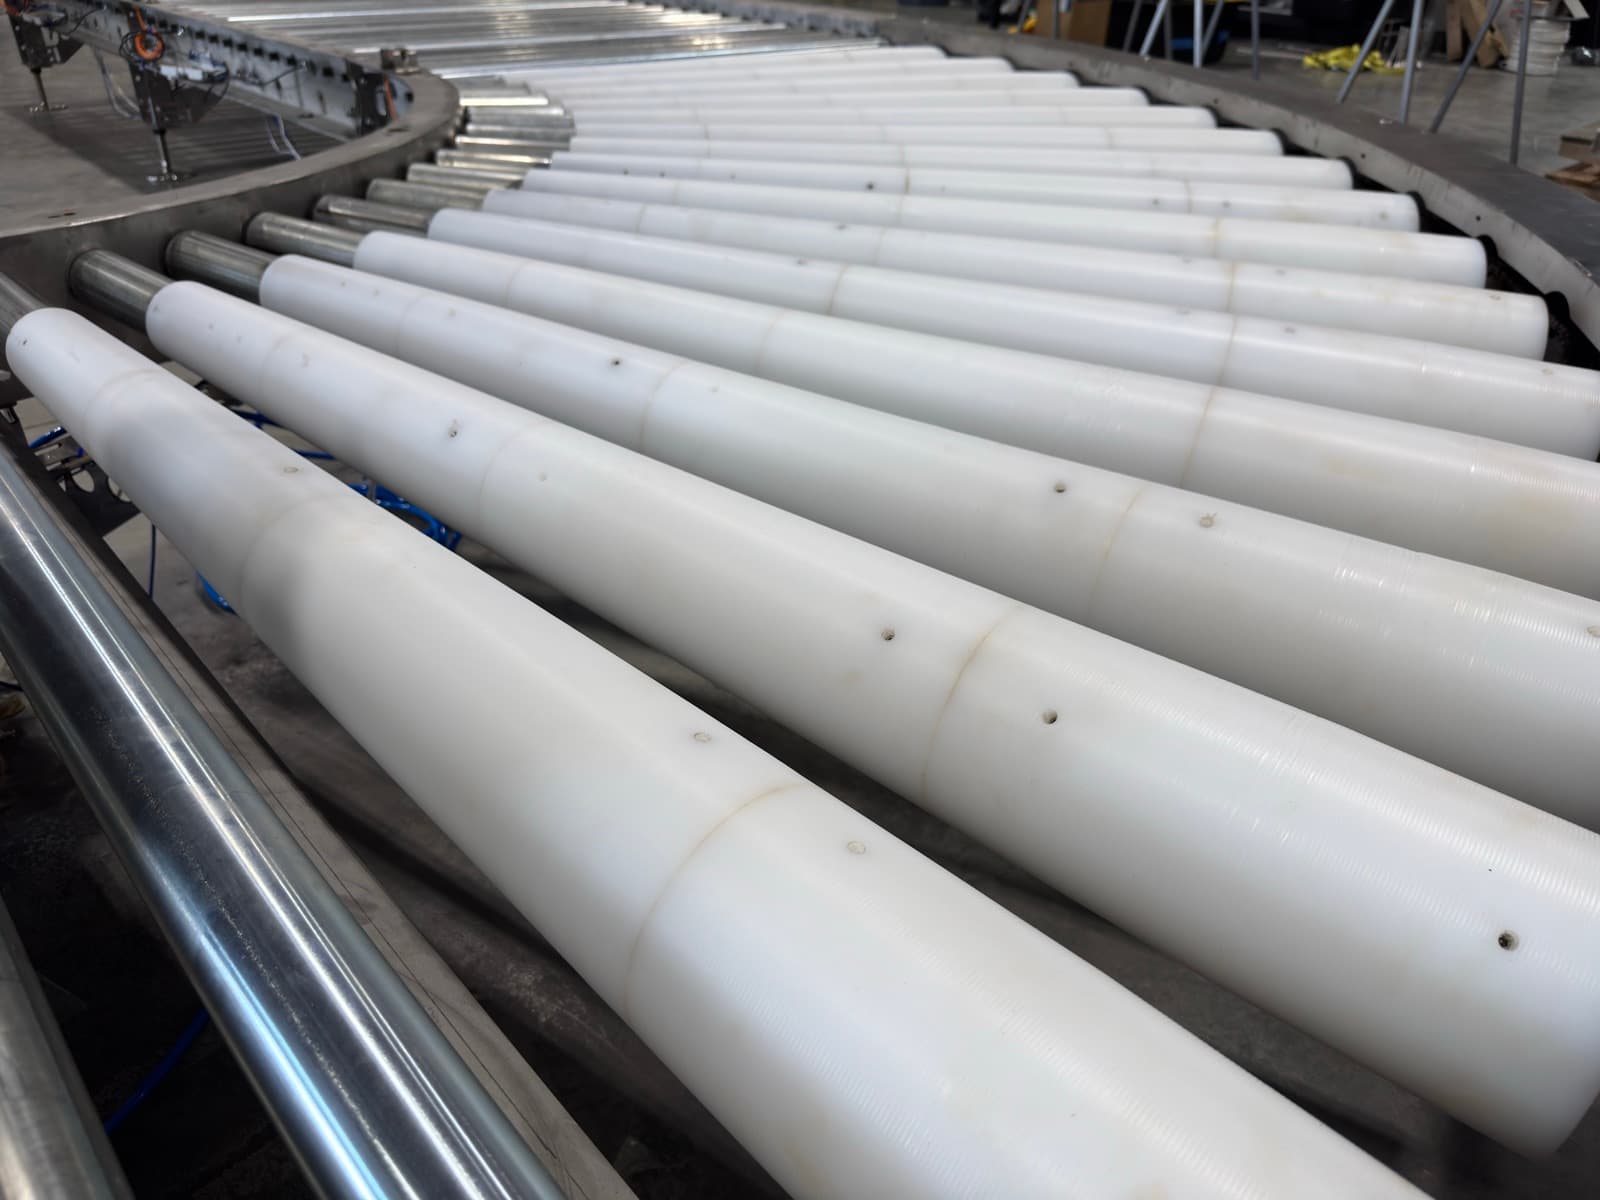
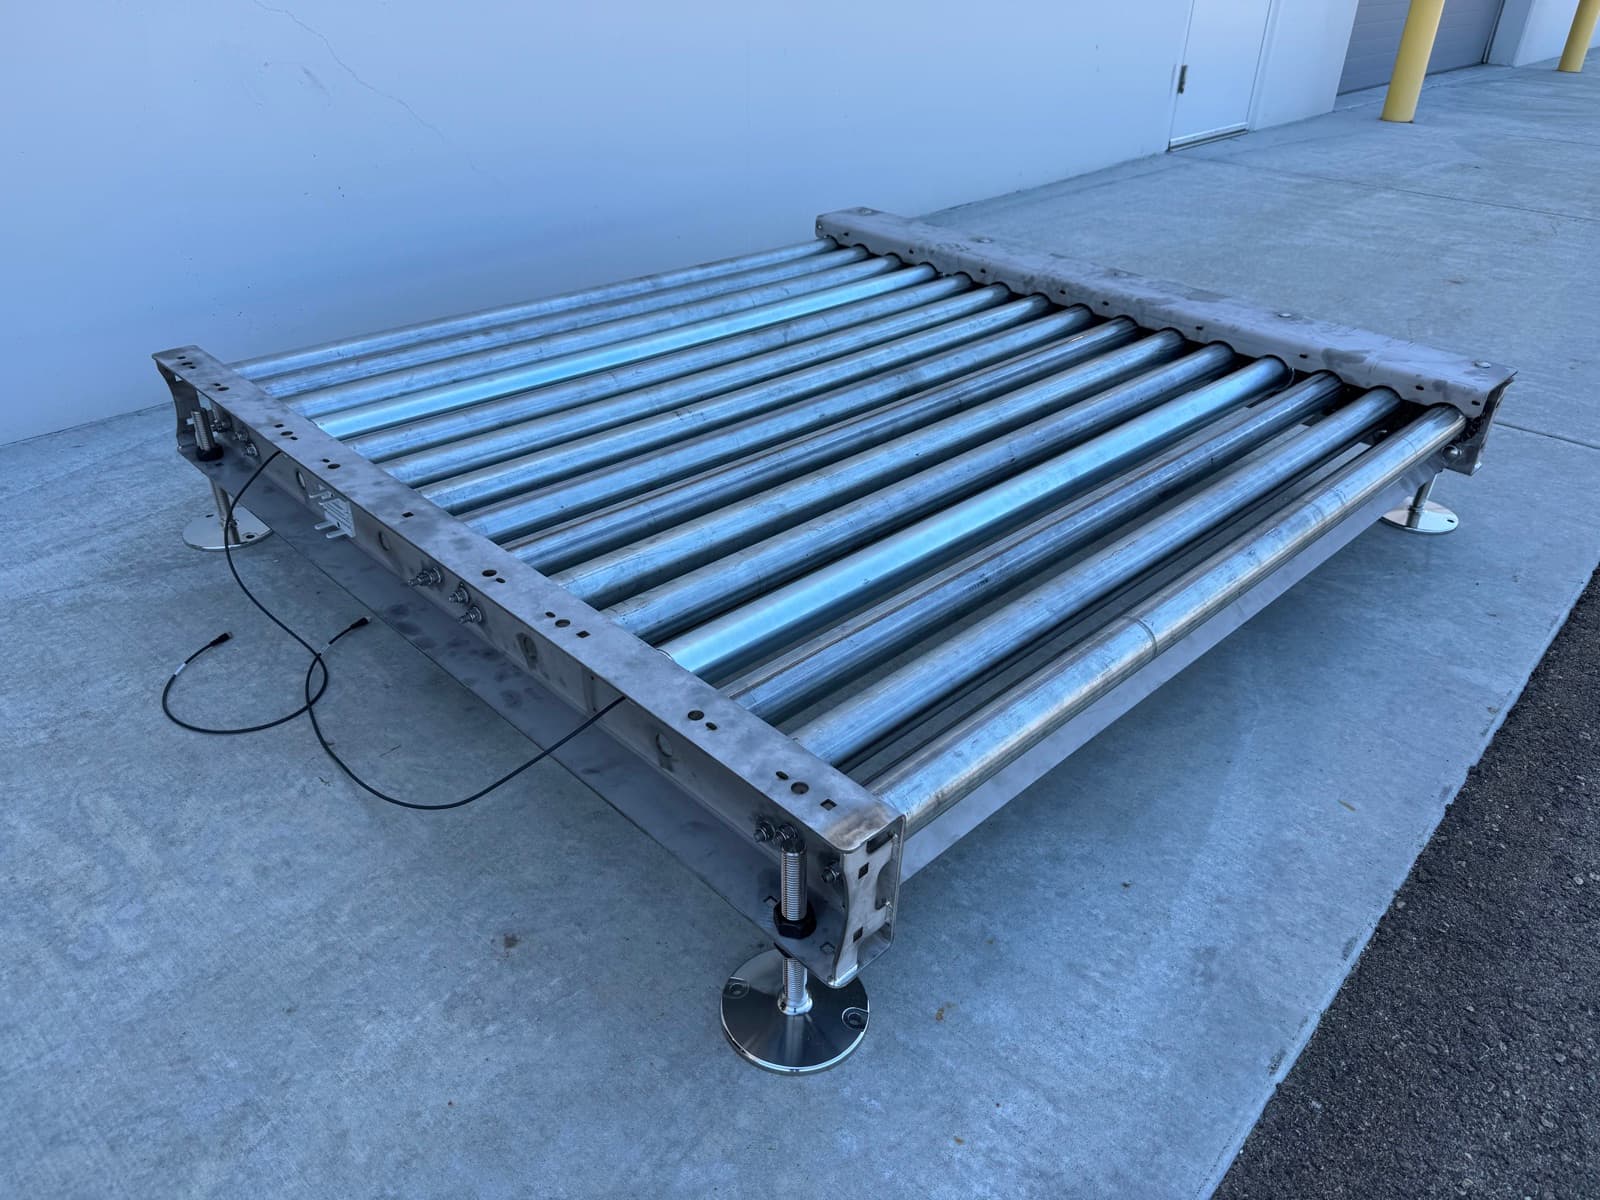
AQS conveyor systems installed across dairy, protein, bakery, and frozen food production facilities.
Where It Fits in the Line
See how this solution integrates into real production line configurations. Explore AQS products in this line.
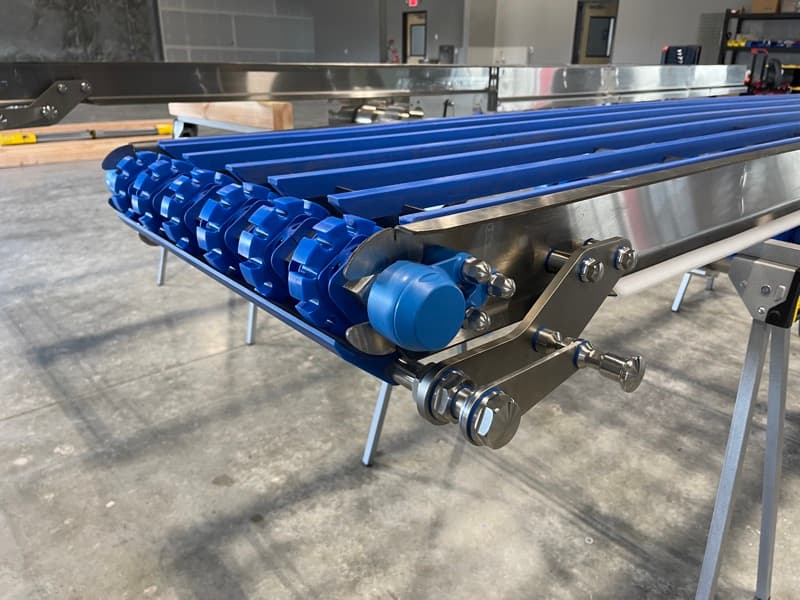
One line, several conveyor jobs: belt conveyors for transport between process stages, 24V MDR for zero-pressure case accumulation, stainless chain for full pallet weight. AQS builds the whole path, so every segment shares the same welded, washdown construction and the same controls.
Tell us about your line
Send us the product, the rate, the room it runs in, and how it gets washed down. An AQS engineer comes back with a layout sketch and a budgetary range — no catalog, no sales script.
Tell Us About Your Line →